Home Industry What Is an Automobile Electronic Control Module in Modern Vehicle Electronic Systems?

What Is an Automobile Electronic Control Module in Modern Vehicle Electronic Systems?

by workdailyfilm
0 comment

An automobile is no longer controlled primarily through mechanical connections. Sensors continuously collect information about vehicle conditions, software interprets that information, and electronic systems issue commands to steering, propulsion, braking, body functions, and other subsystems.


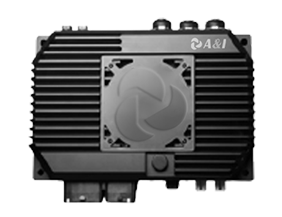
At the center of this process is the automobile electronic control module, a computing unit that processes inputs and manages specific vehicle functions.
 

banner

Understanding its role requires looking beyond the term ECU. Modern vehicles may contain numerous electronic controllers, while newer architectures increasingly consolidate functions into more powerful computing platforms.


Archimedes Innovation’s Poseidon Domain Controller illustrates this transition toward integrated vehicle electronics, where centralized processing can coordinate multiple functions through a broader system architecture.


An Electronic Control Module Is a Vehicle Decision Point


An electronic control module receives information, executes programmed logic, and produces outputs for other vehicle components. Inputs can originate from sensors measuring conditions such as speed, position, temperature, pressure, or system status. Outputs may control actuators or communicate commands to other electronic units.


The basic sequence is therefore straightforward: sense, process, decide, and control. A module continuously repeats this cycle while the vehicle is operating.


Traditional electronic architectures often distribute these responsibilities among dedicated ECUs. One controller might manage an individual subsystem while another handles a different function. Such distribution can work effectively, but the growing number of electronic features creates increasing requirements for communication and coordination between controllers.


How a Module Turns Vehicle Data Into Commands?


The operation of an automobile electronic control module depends on three fundamental elements: processing capability, software, and communication. Hardware receives electrical or digital signals, the processor applies programmed logic, and the resulting information is transmitted to the relevant vehicle systems.


Communication is particularly important because an individual controller rarely operates in isolation. Vehicle networks allow electronic modules to exchange information so that different systems can respond to the same vehicle state.


A modern controller may therefore serve as both a computing platform and a communication node. Its effectiveness depends not only on processing performance but also on its ability to exchange information reliably with sensors, actuators, and other controllers.


Why Modern Vehicles Need More Integrated Control?


Vehicle electronics have become increasingly complex as manufacturers add advanced driver assistance, automated functions, connected services, digital cockpits, electrification, and increasingly software-defined features. More functions mean more data and more relationships between subsystems.


A highly distributed architecture can result in numerous controllers, wiring connections, communication paths, and software environments. Managing these elements becomes more challenging as vehicle functions become increasingly interconnected.


Domain-oriented architectures address part of this challenge by grouping related functions under more capable computing units. Instead of treating every function as an isolated electronic island, the architecture creates higher-level controllers capable of coordinating multiple systems.


Where the Vehicle Domain Controller Fits?


A vehicle domain controller represents this shift from narrowly focused electronic modules toward centralized or domain-level computing. Rather than handling only one small function, a domain controller can coordinate multiple related vehicle systems through shared processing and communication resources.


Poseidon Domain Controller is designed as a vehicle-domain computing platform for integrated vehicle control. Archimedes Innovation describes the product as supporting vehicle-level applications and interfaces intended to connect different components within the electronic architecture.


The distinction is architectural rather than simply semantic. A conventional ECU is commonly associated with a particular control function, whereas a domain controller can consolidate multiple functions and provide a common computing environment.


Such consolidation can also influence how software is developed and updated. Functions that previously depended on separate controllers can potentially be coordinated through a more centralized software architecture, depending on the vehicle’s design.


What Engineers Need From Centralized Vehicle Control?


Centralization changes the engineering priorities. Processing capability matters because one controller may handle significantly more workloads. Communication also becomes critical because the controller can sit between multiple vehicle subsystems.


Interfaces, computing resources, real-time behavior, thermal characteristics, reliability, and software architecture all need to match the intended vehicle application. The controller must also operate within the electrical and environmental conditions expected inside the vehicle.


Poseidon provides an example of a controller designed around vehicle-level integration rather than a single isolated function. Its product architecture reflects the need for modern vehicles to connect computing, communications, and control within a more unified electronic platform.


The selection process therefore starts with the vehicle architecture. Engineers need to determine which functions will remain distributed, which can be consolidated, how data will move between systems, and what processing and interface resources the central controller must provide.


From Individual ECUs to Coordinated Vehicle Intelligence


The importance of an automobile electronic control module lies in its ability to turn vehicle information into controlled action. In a traditional architecture, that role may belong to a dedicated ECU responsible for a specific subsystem. In newer architectures, increasingly capable computing platforms can coordinate several functions across a broader domain.


Archimedes Innovation positions its Poseidon Domain Controller within this evolution toward integrated vehicle computing, providing a platform for applications that require centralized processing and communication.


The result is not simply fewer electronic boxes. A domain-oriented architecture changes where decisions are made and how information is shared across the vehicle. That can provide a foundation for coordinating increasingly software-driven functions while reducing the fragmentation associated with highly distributed electronics.


While electronic control modules remain essential, the key consideration for automotive OEMs and system developers lies in how to properly allocate their respective functional responsibilities.


As vehicle systems become more interconnected, the traditional standalone controller is increasingly complemented, and in some cases replaced, by domain-level computing.


This shift makes the electronic control module an important building block in the transition from distributed vehicle electronics toward coordinated, software-driven vehicle intelligence.

You may also like

Leave a Comment

Soledad is the Best Newspaper and Magazine WordPress Theme with tons of options and demos ready to import. This theme is perfect for blogs and excellent for online stores, news, magazine or review sites.

Buy Soledad now!

Edtior's Picks

Latest Articles

Contact cement manufacturers often need to balance viscosity, flow, wetting, and application behavior when adjusting an adhesive system for different application methods. When a formulation needs to be thinned or its rheological behavior adjusted, the choice of rosin ester tackifier should be considered together with the polymer base, solvent system, and other formulation components. Rather than treating a rosin ester as a standalone solution for viscosity reduction, formulators can evaluate how its documented properties and compatibility with the adhesive system may affect viscosity, flow, tack, and processing behavior. Grade information, physical form, and processing conditions can then provide a basis for further formulation testing. Starting with the Viscosity Requirements of Contact Cement Systems In thinning contact cement systems, the target viscosity should be considered together with the desired flow and application behavior. Brush, roller, and other application methods can place different demands on how easily the adhesive spreads while still maintaining sufficient tack and film-forming behavior. Formulators may therefore establish a target viscosity range and identify the required flow characteristics before comparing rosin ester grades. The effect of a selected grade should then be verified within the complete polymer-solvent-resin system rather than inferred from the resin’s specification alone. The first step is usually to identify which material characteristics need to be confirmed. Depending on the grade, supplier documentation may provide information such as softening point, acid value, color, and other applicable specifications. Reviewing these details alongside the manufacturer’s internal requirements gives technical and purchasing teams a more structured starting point. Solvent-borne contact cement systems can also involve different raw-material combinations. Rather than assuming that every rosin ester grade will behave in the same way, formulators can identify the polymer and solvent system involved and then discuss relevant material options with suppliers. This approach keeps the initial selection process focused on documented information rather than unsupported assumptions. For procurement teams, this early screening can also reduce unnecessary supplier comparisons. A clear list of required specifications, physical form, packaging, and purchasing conditions allows potential raw-material sources to be evaluated on a consistent basis. The final selection can then proceed according to the manufacturer’s established technical and approval procedures. Reviewing Rosin Ester Grades for Processing Requirements Rosin ester resins are available in different grades, and differences in resin properties can influence how a grade behaves within a particular adhesive formulation. When rheology and viscosity are important formulation targets, formulators can consider documented properties such as softening point, acid value, color, and other applicable specifications together with the polymer and solvent system. These parameters should not be treated as direct indicators of final adhesive viscosity; instead, they can help formulators identify suitable candidates for comparative formulation trials. Evaluating the resulting viscosity, flow, application behavior, and tack can provide a more practical basis for assessing the role of each rosin ester grade. Physical form is another practical issue for contact cement manufacturers. Solid resins may be supplied in forms such as flakes, pastilles, or other formats depending on the supplier and product grade. Confirming the actual supplied form before purchasing allows production and warehouse teams to assess whether existing receiving and material-handling procedures are suitable. Packaging can affect the practical side of raw-material handling as well. Buyers may need to confirm package type, unit weight, labeling, and storage guidance before placing recurring orders. Clear information at this stage can help the receiving facility prepare for incoming materials without making assumptions about how a particular resin should be handled. Processing conditions can also affect how a contact cement formulation is handled after viscosity or rheological adjustments are made. Mixing efficiency, temperature, solvent addition, resin incorporation, and material-transfer conditions may influence the consistency of the adhesive during production and application. Different plants may therefore require separate evaluation even when the same rosin ester grade is being considered. Supplier documentation can provide a reference for raw-material handling, while manufacturers should verify viscosity, flow, and processing behavior under their own production conditions. Connecting Resin Selection with Adhesive System Requirements The role of a rosin ester tackifier should be considered in relation to the complete contact cement formulation, particularly when the objective is to adjust viscosity or rheological behavior. Different polymer bases, solvent combinations, and resin concentrations can produce different formulation responses, so a grade that performs acceptably in one system may require separate evaluation in another. Formulators can compare candidate rosin ester grades by monitoring changes in viscosity, flow, tack, and application behavior under their intended formulation conditions. Supplier discussions can then focus on grades with documented characteristics relevant to the specific adhesive system. Compatibility should be treated as a selection question rather than a universal assumption. A material suitable for one adhesive system may not automatically be appropriate for another. Reviewing available product information and discussing the intended application with the supplier can help technical teams determine which candidates should proceed to their own internal evaluation. Long-term processing conditions may also form part of the initial discussion. Manufacturers operating regular production lines can identify the temperature range, handling conditions, and material-transfer requirements relevant to their facility. These details give suppliers useful context when presenting available rosin ester options without turning the sourcing discussion into a fixed formulation recommendation. Documentation remains particularly useful when several grades appear similar at first glance. Comparing technical data sheets, product identification, packaging information, and supply conditions can help purchasing and technical teams distinguish between candidates. Keeping these records organized also provides a clearer reference when a selected grade moves from initial sourcing into recurring procurement. Building a More Practical Rosin Ester Sourcing Process Once a suitable group of grades has been identified, manufacturers can move from technical screening toward supplier evaluation. Relevant questions may include available grades, minimum order quantities, packaging formats, documentation, lead times, and delivery arrangements. These factors are especially useful when the material will become part of a recurring raw-material purchasing program. Batch information can also be discussed with the supplier according to the buyer’s internal requirements. Purchasing and technical teams may need consistent product identification and documentation for incoming materials. Clear communication around these requirements helps both parties understand what information should accompany regular orders. KOMO provides industrial customers with product information covering rosin ester grades, specifications, physical forms, packaging, and supply requirements. For contact cement manufacturers evaluating raw-material options, these discussions can help clarify which product information should be reviewed before establishing a regular purchasing arrangement. Supplier communication can become particularly valuable when a manufacturer operates multiple production lines or purchasing locations. Different facilities may have different receiving procedures, packaging preferences, or delivery schedules. Discussing these practical points in advance gives the purchasing team a clearer basis for coordinating future orders. Industry professionals can use exhibitions to discuss raw-material questions directly with suppliers and compare material options against their technical and sourcing requirements. For manufacturers assessing rosin ester options for contact cement, CHINACOAT 2026 provides an opportunity for adhesive manufacturers, formulators, and procurement professionals to speak with KOMO about available rosin ester grades, documented specifications, physical forms, application and processing considerations, packaging formats, and ongoing supply arrangements. Face-to-face discussions can help clarify material and sourcing information before manufacturers proceed with their own internal evaluation. CHINACOAT 2026 will take place November 11–13, 2026, at the China Import and Export Fair Complex in Guangzhou, with KOMO at Booth 5.2 C47.

All Right Reserved. Designed and Developed by workdailyfilm.